If you’re a welding fabricator, job shop, or anyone relying on consistent, high-quality welding wire for operations, the performance of your winding machinery isn’t just a secondary detail—it’s the backbone of your entire production line. As a supplier of welding wire winding machinery, I’ve spent the last 12 years walking clients through pre-use testing that skips the guesswork and catches issues before they grind work to a halt. I’ve seen new machines arrive on-site with misaligned spindles that ruin spool tension, and I’ve also fixed small, easy-to-miss oversights that cause 30% more downtime in the first month of operation. Over time, I’ve refined a step-by-step testing process that works for every type of wire winding equipment we sell, from compact bench-top units for small production runs to heavy-duty industrial models that wind 500kg spools at 120 meters per minute. This isn’t just “turning the machine on and pressing go”—it’s a structured, safety-first test that validates every core function of the equipment before it touches critical production wire. Before we dive into the steps, let’s set a baseline: welding wire has very specific requirements for tension, alignment, and spool integrity. Too much tension stretches the wire, leading to inconsistent arc performance and potential breakage during welding. Too little tension causes tangles, bird nests, and uneven spool fills that waste material and time. My process is built to confirm our machines deliver on those requirements, and it works for every client regardless of their operation size. Welding Wire Winding Machinery

The first test I walk clients through is a static pre-start inspection and baseline check—do this before you even plug the machine in, because safety and part condition start before power is applied. This is where most new operators skip steps, but it’s the most important foundation. First, check the machine’s structure for any signs of shipping damage: when we wrap and ship winding equipment, we use heavy-duty crating, but sometimes forklift mishandling can bend the frame, misalign the spindle mount, or loosen tension springs. Grab a level and check both the machine’s main frame and the spindle axis—they should be perfectly horizontal. A 1-degree tilt in the spindle can throw wire tension off enough to cause tangles during the first run. Next, inspect all contact points that wire will touch: the guide rollers, tension discs, and any bushings along the winding path. Look for sharp edges, burrs, or grease residue that could stick to soft welding wire (like aluminum or flux-cored wire) and cause surface imperfections. For stainless steel welding wire, even a tiny burr can nick the surface, leading to corrosion or breakage during use. I always tell clients to run a clean rag along every contact point here—if it picks up metal shavings or dirty grease, that’s a sign something is misaligned inside the machine. Finally, test the emergency stop button. This is non-negotiable: press it, confirm the machine cuts all power instantly, reset it, and check that the motor and controls turn on smoothly. I’ve seen a client skip this check, and when a tangled wire caught on a guide roller mid-test, they couldn’t stop the machine fast enough to damage a $2,000 roll of steel wire and put a 3-day delay on their project. Small, simple checks prevent huge headaches.
Once the static inspection is clear, move on to the next test: motor and speed accuracy testing. The winding machine’s motor is what drives the wire feed, so if its speed doesn’t match the programmed setting, the entire winding process will be off. Start by plugging the machine in, but leave all wire spools and feeders disconnected for this test—we want to isolate the motor’s performance. Set the machine to its standard operating speed (for most industrial models, that’s 80-120 m/min; for bench-top units, it’s 20-50 m/min). Run the motor for 10 seconds, then stop. Now, use a handheld tachometer to measure the spindle’s rotational speed, and cross-reference it with the machine’s control panel readout. A difference of more than 5% here is a red flag—that means the motor’s encoder is misaligned, or the control panel calibration is off. We calibrate every machine before shipment, but shipping vibrations can shift these settings. Next, test speed consistency over a longer period: run the motor for 5 minutes at a steady speed, checking the tachometer every 60 seconds. If the speed jumps up or down more than 10 m/min during this test, there’s a problem with the motor’s power supply or the drive system that needs fixing before you run actual wire. For machines with variable speed settings, test the full range: slowest speed (for small gauge wire that needs delicate handling) to maximum speed, confirming the machine accelerates smoothly without jerking or stalling. Jerking during acceleration is a common issue with new machines, and it can cause the wire to stretch even when you have tension dialed in. We had a client a few years ago who missed this test, and when they switched from 0.8 mm to 1.6 mm wire, the machine’s acceleration jerk caused 47 breaks on a single 250kg spool. That test would have caught that issue in 5 minutes.
After motor and speed checks, move on to the most critical test for welding wire: tension testing. This is where a lot of third-party testers cut corners, but it’s the reason our machines are designed the way they are. Welding wire tension isn’t a “set it and forget it” number—different wire types, gauges, and spool sizes require different tension levels. For example, 0.8 mm flux-cored wire needs 0.5-1.0 kg of tension, while 2.0 mm solid steel wire needs 1.5-2.5 kg to avoid sag or tangles. To test tension accurately, you’ll need a simple digital tension gauge (most metalworking suppliers carry these for under $100—no need for expensive industrial equipment here). First, thread a 1-meter length of clean, uncoiled welding wire (use the same wire you plan to wind in normal operation) through the machine’s guide path, between the tension discs, and secure it to a fixed point (like a wall or heavy workbench) so the wire is taut but not stretched. Hold the tension gauge horizontally at the point where the wire would be fed into the winding spindle, and pull steadily until the wire starts to move. The gauge will show the tension required to pull the wire through the machine—this should match the recommended tension for your wire type within 10%. If the tension is too high, that means the tension spring is over-adjusted, or the guide rollers are rubbing too tightly against the wire. If it’s too low, the spring is under-adjusted, or there’s too much slack in the guide path. Once you set the correct tension, run the machine for 10 minutes winding a 500g test spool of your wire, then stop and re-test tension at different points along the spool (the top, middle, and bottom). If the tension changes as the spool fills, that means the spindle’s pressure mechanism is misaligned, or the wire is slipping unevenly between the tension discs. I always advise clients to do this test with their actual production wire—don’t use a cheap test wire, because different wire coatings and gauges will interact with the machine’s parts differently. We had a client who used a cheap steel test wire for initial testing, and when they switched to their regular aluminum wire, the tension was 30% too low, leading to a full day of tangles and wasted material. Using the right wire for testing avoids that.
Next, test the winding pattern and spool fill accuracy. A winding machine’s job isn’t just to wind wire—it’s to wind it in a neat, consistent pattern that avoids tangles during unwinding. Most modern machines use a traversing mechanism that moves the guide wire back and forth evenly across the spool flange. To test this, wind a full 10kg test spool at your normal production speed, then inspect the pattern. The wire should lay side-by-side with no overlapping gaps, no hills or valleys, and no wire extending over the spool flange (called “flange breakout,” which causes tangles when the wire is fed into the welding gun). If you notice overlapping, that means the traversing mechanism’s gear is worn (a rare issue with new machines, but possible if shipping damaged the gear housing) or the traverse speed is not matched to the spindle speed. If there are gaps between wire layers, the traverse speed is too fast or too slow. Another thing to check: the spool’s end stop. When the machine reaches the end of the spool flange, it should automatically reverse direction smoothly, not jerk. Jerking at the end stop can cause the wire to bunch up or break. I also tell clients to test the spool’s weight and capacity accuracy. Most industrial machines have a load cell or weight sensor that can automatically stop winding when the spool reaches the desired weight. We calibrate these before shipment, but again, shipping vibrations can shift the calibration. To test this, wind a spool to its rated capacity (e.g., 250kg), then weigh it manually. The machine’s weight reading should be within 1% of the actual weight. If it’s off by more, that means the load cell needs re-calibration, which is a simple fix we can walk you through over a call. This test saves you from winding spools that are under or over capacity, which leads to wasted wire or wasted production time because the spool runs out mid-job.
Finally, safety and long-run testing. This is the test that tells you if the machine will hold up during a full day of production, not just a 10-minute trial run. Safety features should be the most reliable part of any winding machine, so test all safety interlocks: the guard over the tension discs, the cover over the traverse mechanism, and the emergency stop. Open the guard while the machine is running—if the interlock doesn’t cut power instantly, that’s a critical safety issue. For long-run testing, wind a full production spool (or multiple small spools) at your normal speed and tension, and watch for any issues over 1 hour of continuous operation. Listen for unusual noises: grinding, squealing, or rattling, which can mean a loose part or misaligned bearing. Check the wire for any surface damage, nicks, or bends as it comes off the machine—even a tiny nick here will cause problems during welding. Also, check the machine’s temperature: touch the motor and bearing housings after 1 hour of running. If they’re too hot to touch comfortably (around 120°F or 49°C), that means there’s friction or a power issue that will shorten the machine’s lifespan. We had a client who skipped this test, and after 3 months of running 8 hours a day, their bearing seized up, costing them $1,200 in replacement parts and 2 days of downtime. That 1-hour test would have caught the overheating bearing early, for a $50 repair part instead of a $1,200 replacement.
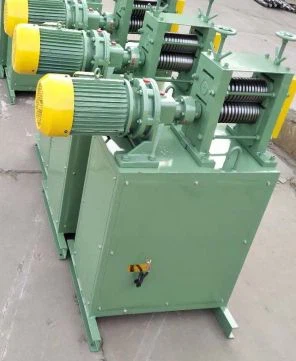
I’ll be honest—this process takes about 2 hours for a full machine, plus another 2 hours if you’re using actual production wire, but it’s way faster than fixing a breakdown mid-production or wasting hundreds of dollars on bad spools. The biggest mistake I see new operators make is rushing through pre-use testing to get the machine online faster, but that’s false economy. As a supplier, our goal isn’t just to sell you a winding machine—it’s to make sure it works for you, long after the installation. If you’re running through these tests and notice any discrepancies, don’t hesitate to reach out. We provide free pre-use troubleshooting support for every machine we sell, and we can walk you through calibrations or part adjustments over a call, or send a service technician out if needed. Don’t leave the performance of your welding wire and your production line to chance—take the time to test your winding machine properly before you start running critical jobs.
Other Auxiliary Equipment References:
- American Welding Society. (2021). Welding Wire Handling and Storage Best Practices. AWS D1.1 Standard, Structural Welding Code.
- Machinery Lubrication Magazine. (2022). Pre-Startup Testing for Industrial Processing Equipment. Volume 12, Issue 4.
- International Organization for Standardization. (2019). Winding Machinery Performance and Safety Standards for Metalworking. ISO 18425:2019.
- Manufacturing Engineering Association. (2023). Preventive Maintenance and Pre-Use Testing Protocols for Welding Equipment. MEA Technical Report 23-07.
Three Water Machinery Co., Ltd.
Three Water Machinery Co., Ltd. is one of the most reliable manufacturers and suppliers of welding wire winding machinery in China. With abundant experience, we warmly welcome you to buy advanced equipment for sale here and get quotation from our factory. Contact us for more details.
Address: No.15, Jiaye Road, Liuanzhuang Industrial Park, Beichen District, Tianjin, China
E-mail: sales@eqet.com
WebSite: https://www.eqet.com/
