If you’ve ever worked with heavy machinery, construction equipment, or automotive parts, you know how critical pin shafts are to keeping everything connected. As someone who’s supplied pin shafts for over 12 years, I’ve seen firsthand how a small crack in these components can turn into a major breakdown—one that costs clients thousands in downtime, repairs, and even safety incidents. Last year, a construction customer called me in a panic because three of our pin shafts developed cracks mid-project on a bridge job. We fixed the issue on-site that same day, but it got me thinking: there’s no single solution to preventing pin shaft cracking. It’s a combination of smart design, careful material selection, precise manufacturing, proper installation, and regular maintenance. If you’re relying on pin shafts for heavy-duty applications, here’s what we’ve learned at our shop over the years to stop cracks before they start. Pin Shaft
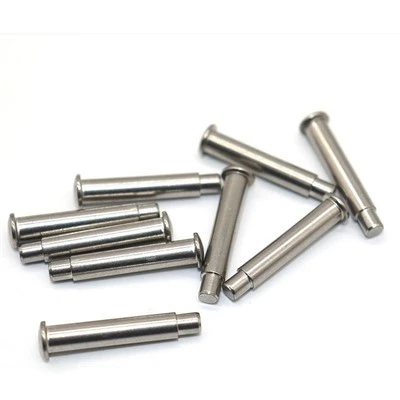
First and foremost, pin shaft cracking almost always ties back to material selection and how it’s processed. When I started in this business, we used generic carbon steel for every order, and we dealt with way more failures than we do now. Now, we match the material to the exact load, environment, and application. For example, a pin shaft for a farm tractor’s hitch gets exposed to dirt, moisture, and constant shock loads, so we use a medium-carbon alloy steel like 4140. This steel has better tensile strength and impact resistance than plain carbon steel, which means it can handle sudden jerks and heavy weights without bending or cracking. For applications in saltwater or chemical plants, we switch to a stainless steel like 316, which has corrosion resistance that prevents rust from eating into the shaft and creating stress points. The key here is avoiding overloading the material—using a steel that’s too soft for the job might bend before it cracks, but a steel that’s too brittle will crack under even moderate stress. We also pay close attention to heat treatment, because that’s where a lot of our competitors cut corners. If a pin shaft isn’t properly quenched and tempered, it’s either too soft (prone to bending) or too hard (prone to cracking). Last month, a client sent back a batch of pin shafts from another supplier that cracked during installation; when we tested the hardness, it was 5 points over the recommended range for that application. We always test each batch with a Rockwell hardness tester to make sure it’s within the right zone—hard enough to resist wear, but tough enough to absorb shock. We also avoid residual stresses from machining by stress-relieving the shafts after cutting and turning. Residual stresses are like hidden time bombs in metal; they build up during manufacturing and can cause cracks even if the shaft is installed correctly. By heating the shaft to a specific temperature and letting it cool slowly, we eliminate those stresses before they become a problem.
Next, the design of the pin shaft itself plays a huge role in preventing cracking. A lot of engineers focus only on the diameter and length, but the small details around the pin’s ends and shoulders are where cracks most often start. We once had a client with a conveyor system where pin shafts kept cracking at the shoulder—where the thicker part of the shaft meets the thinner end that fits through the hole. The original design had a sharp, right-angle shoulder, which created a stress concentration point. When we redesigned the shoulder with a smooth radius, using a fillet transition that was at least twice the diameter of the pin, the cracking stopped entirely. Stress concentrations are where the metal is under far more force than the surrounding area, so even a tiny notch, scratch, or sharp corner can turn into a crack. That’s why we also make sure to deburr all edges of the pin shaft after machining. Burrs are those sharp, tiny metal bits left from cutting, and they’re almost impossible to spot with the naked eye, but they act like tiny stress raisers. We use a vibratory tumbler to polish the edges of every pin shaft we ship, so there are no burrs or sharp corners. Another design mistake we see a lot is using a pin shaft that’s too small for the application. If a pin is only 10mm in diameter for a load that requires 14mm, it will bend and crack under pressure. We use finite element analysis (FEA) for all our custom orders to map out where the stress points will be, so we can adjust the diameter, length, or even the material before we start production. For example, a pin for a excavator’s bucket might have a small oil hole for lubrication, but if that hole is placed too close to the shoulder, it creates a stress point. We now place all oil holes at least 5 times the hole’s diameter away from any load-bearing edges to avoid this.
Manufacturing processes are another make-or-break factor for pin shaft durability. Even with the right material and design, a bad machining job will lead to cracking. We’ve invested in CNC lathes and mills that give us precision within 0.001 inches, which is non-negotiable. If a pin shaft is machined unevenly, the thickness varies, and some areas are under more stress than others. We also avoid cold forming for high-load pin shafts, because that process can introduce microcracks just under the surface of the metal. Microcracks are too small to see, but they grow over time until they turn into full cracks. For low-load, decorative pin shafts, cold forming is fine, but for construction and industrial uses, we use hot forging, which shapes the metal at high temperatures and creates a more uniform grain structure. A uniform grain structure means the metal is stronger along all axes, so it resists cracking better than a metal with uneven grain from cold forming. We also do non-destructive testing (NDT) on all our high-volume orders. Our NDT team uses magnetic particle testing, which detects tiny surface and subsurface cracks that aren’t visible to the naked eye. Last quarter, we found three microcracks in a batch of 500 pin shafts; it turned out there was a small flaw in the raw steel we’d gotten from a new supplier. We stopped working with that supplier immediately, and now we test every batch of incoming steel before we even start machining. That’s the kind of quality control that sets us apart from smaller suppliers—we don’t assume the material is perfect, we prove it.
Proper installation and lubrication are steps that clients often overlook, but they’re just as important as anything we do in our shop. I can’t tell you how many times a client blames a cracked pin shaft on “bad material” when the real issue is that they installed it incorrectly. For example, if you hammer a pin shaft into place instead of using a press, you’re introducing impact stress that can cause microcracks. We include detailed installation instructions with every order, and we also hold free workshops for our regular clients to walk them through proper installation. The key here is making sure the pin fits snugly in both parts it’s connecting—too loose, and it moves back and forth, causing wear and stress; too tight, and you’re forcing it, creating damage. We recommend using a press fit for high-load applications, with a clearance of no more than 0.002 inches, to ensure it’s secure without being forced. Lubrication is another big one. Pin shafts that rotate or move need lubrication to reduce friction, and friction generates heat, which weakens the metal and can cause thermal cracking. We recommend using a high-pressure, extreme-pressure (EP) grease for heavy-duty applications, and we also add a small grease fitting to all pin shafts for industrial machinery. We even pre-lubricate every pin shaft we ship, so clients don’t have to go through the trouble of greasing them before installation. If a client tells us they’re having cracking issues, the first question we ask is whether they’re following our lubrication guidelines—more often than not, that’s the root cause.
Finally, regular maintenance is the last line of defense against pin shaft cracking. Even the best pin shafts will wear out over time if they’re not checked. We advise clients to inspect their pin shafts every 100 working hours for heavy machinery, or every 50 hours for equipment that’s in constant use. During an inspection, you’re looking for small signs: surface scratches, discoloration, a slight bend, or any play when you wiggle the shaft. We also recommend using a dye penetrant test annually to check for hidden cracks. Dye penetrant is a simple, non-toxic liquid that seeps into any surface cracks, and you can wipe off the excess and see the cracks clearly with a UV light. Last year, a trucking client didn’t inspect their pin shafts for a year, and a crack that started small on their trailer’s hitch grew until the pin shaft broke on the highway. No one was hurt, but the trailer was totaled, and they had to pay for a tow and repairs that would have cost a fraction if they’d done regular inspections. We now offer a maintenance check service for clients within a 50-mile radius, and we also send digital inspection checklists to all our customers so they can do their own checks if they’re far away. It’s not just about selling pin shafts—it’s about making sure they work for years, and that means supporting our clients long after delivery.
At the end of the day, preventing pin shaft cracking isn’t a secret—it’s a combination of attention to every detail, from material selection to maintenance. We’ve spent years refining our processes because we care about our clients’ business; when their equipment is down, we’re the ones they call, and we don’t want to let them down. If you’re dealing with pin shaft cracking issues, or you need a reliable supplier for high-quality pin shafts for your application, we’re here to help. We can work with you to design the right pin shaft for your needs, test every batch for flaws, and offer guidance on installation and maintenance to keep your equipment running smoothly. Don’t let small cracking problems turn into costly breakdowns—reach out to our team to discuss your pin shaft requirements, and we’ll make sure you get a solution that lasts.
Rivet References
- Ashby, M. F., & Jones, D. R. H. (2012). Engineering Materials 1: An Introduction to Properties, Applications, and Design. Butterworth-Heinemann.
- Kalpakjian, S., & Schmid, S. R. (2020). Manufacturing Processes for Engineering Materials. Pearson.
- American Society of Mechanical Engineers (ASME). (2019). B106.1M-2019: Design of Transmission Shafting. ASME International.
- Davies, J. R. (2003). Alloyer Selection, Volume 2: Corrosion. ASM International.
- NPTEL. (2018). Manufacturing Technology: Metal Forming. Indian Institute of Technology Kharagpur.
Wuyuan Jieyi Automotive Electrical Appliance Co., Ltd.
As one of the most professional pin shaft manufacturers and suppliers in China, we’re featured by quality products and good service. Please rest assured to wholesale bulk durable pin shaft in stock here from our factory. We also accept customized orders.
Address: No. 7 Likeng Road, Industrial Park Wuyuan County, Shangrao City, Jiangxi Province
E-mail: wyjydqz@163.com
WebSite: https://www.wyjydq.com/
